[language-switcher]

2026 Best Copper Stamping Machine for Global Buyers

Choosing the 2026 best Copper Stamping Machine requires more than comparing tonnage, speed, or purchase price. Global buyers need equipment that performs consistently under real production pressure. A machine may stamp thin copper terminals beautifully, yet struggle with thicker busbars, narrow bends, or complex progressive dies. That difference matters.

Dr. Taylan Altan, a leading authority in sheet-metal forming, has emphasized that “the quality of a stamped part depends on the process, the material, and the tooling—not on press tonnage alone.” His observation remains highly relevant for copper applications. Copper conducts heat quickly, marks easily, and can deform when clearance, lubrication, or die alignment is poorly controlled. A reliable machine should therefore offer stable slide motion, precise pressure control, suitable feed accuracy, and accessible maintenance points. Small details count. Even a loose guide rail can create burrs across thousands of terminals.

This guide evaluates Copper Stamping Machine options through practical criteria, including copper grade compatibility, stroke length, production speed, automation readiness, energy use, operator safety, and supplier support. It also considers documentation, spare-part availability, testing records, and quality-control evidence. These factors often reveal more than polished brochures. No machine wins every application. That is an uncomfortable truth. Some manufacturers publish impressive figures without explaining testing conditions, die design, or material thickness. Buyers should question those gaps before making a global purchase. The strongest choice is not always the fastest press. It is the machine that delivers repeatable parts, manageable operating costs, and dependable support throughout its working life.
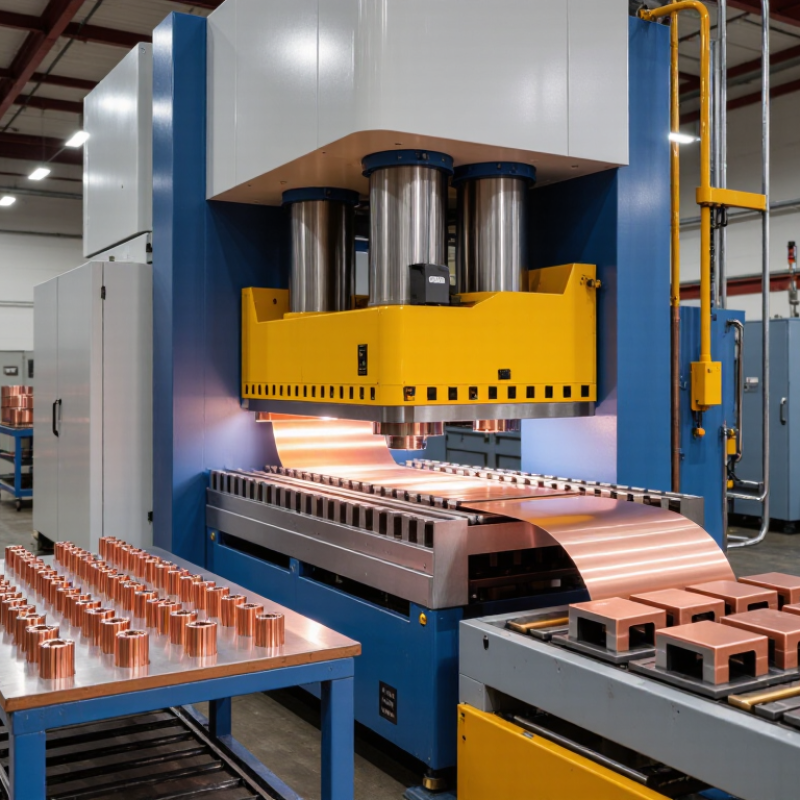
2026 Best Copper Stamping Machine for Global Buyers

What Is a Copper Stamping Machine and How Does It Work?

A copper stamping machine converts flat copper sheet or coil into precise parts through controlled pressure. A feeder moves the material forward, while a punch enters a hardened die. The operation may pierce, cut, bend, or draw the copper. High electrical conductivity makes copper valuable for terminals, busbars, connectors, and heat-transfer components.

The machine’s key variables are press force, stroke speed, die clearance, and feed accuracy. Too little clearance can tear the edge. Too much may create burrs and weak profiles. The USGS Mineral Commodity Summaries 2025 estimated global copper mine production at about 22 million metric tons in 2024. This scale supports continued demand for efficient, repeatable forming equipment. In real workshops, the first setup is rarely perfect. Material temper, thickness variation, and tool wear still require practical adjustment.

Tips: Check copper thickness before choosing tonnage. Ask for trial stamping with your actual alloy and geometry. Inspect burr height, flatness, and springback. A slower cycle can sometimes produce better parts and fewer die repairs. Report data helps buyers understand market pressure, but it cannot replace a factory test.

Main Types of Copper Stamping Machines for Industrial Production

Main Types of Copper Stamping Machines for Industrial Production

For global buyers, machine selection should match copper thickness, part geometry, and production volume. Mechanical presses use a flywheel and crankshaft to deliver fast, repeatable strokes. They suit terminals, washers, and electrical clips made from thin copper strip. With progressive dies, one coil can pass through several forming stations continuously.

Hydraulic presses generate force through fluid pressure. They offer controlled speed and steady pressure, which helps with deeper forming and thicker copper parts. However, their cycle speed is usually lower. Servo presses use programmable slide movement, allowing precise forming profiles and reduced material stress. They can also lower energy use, but their purchase and maintenance costs may be higher.

Tooling layout creates another practical distinction. Single-station presses work well for prototypes and low-volume orders. Transfer presses move blanks between separate dies, supporting larger or more complex components. Progressive stamping machines combine feeding, piercing, bending, and cutoff operations in one line. This saves labor, but die design becomes demanding.

Check press rigidity, feeder accuracy, die clearance, and scrap removal before ordering. Copper conducts heat quickly, yet burrs can still appear when clearance is poorly adjusted. A common mistake is choosing tonnage only from material thickness. Part shape matters too. I would also request sample runs with the intended copper grade. Small differences in temper can change springback, surface marks, and final dimensions. No machine choice is perfect.

2026 Best Copper Stamping Machine for Global Buyers - Main Types of Copper Stamping Machines for Industrial Production

Machine Type Typical Capacity Range Typical Stroke Rate Suitable Copper Material Thickness Typical Feed and Production Configuration Best Applications Main Advantages Key Limitations
Mechanical Power Press 16–400 metric tons 30–600 strokes per minute, depending on press size, stroke length, and tooling Approximately 0.10–6.00 mm for common copper alloys; actual limits depend on part geometry and die design Manual, straightener-and-feeder, or coil-line operation; available with single-point or double-point frames General blanking, bending, piercing, shallow forming, terminals, brackets, and electrical connector components High production speed, mature technology, comparatively low operating cost, and good repeatability with properly maintained dies Fixed slide motion; less adaptable than servo presses for complex forming sequences and variable-speed operations
High-Speed Precision Press 10–160 metric tons 200–1,500 strokes per minute in specialized high-speed configurations Approximately 0.05–2.00 mm for thin copper strip and precision Electrical Parts High-precision coil feeding, automatic lubrication, die-protection sensors, and progressive-die production Fine-pitch terminals, connector contacts, relay components, lead frames, and miniature electrical parts Very high output, accurate repeatability, and efficient material utilization when matched with progressive tooling Higher tooling and maintenance requirements; sensitive to strip quality, lubrication, alignment, and vibration
Servo Press 30–630 metric tons Programmable; commonly 20–200 strokes per minute for forming work, with higher speeds for lighter operations Approximately 0.20–5.00 mm, depending on copper grade, part depth, and forming load Programmable slide motion, adjustable dwell, variable stroke profiles, and automated coil feeding Complex drawn parts, precision electrical housings, heat-sink components, multi-stage forming, and sensitive copper alloys Flexible slide control, reduced impact during forming, improved control of springback, and potentially lower noise and energy use Higher purchase price and greater control-system complexity than conventional mechanical presses
Hydraulic Press 50–2,000 metric tons or more 5–60 strokes per minute, depending on cylinder size and forming cycle Approximately 0.50–12.00 mm for heavy-gauge copper parts and deeper forming operations Single-station, transfer, or custom tooling; programmable pressure and dwell control are commonly available Deep drawing, heavy-gauge busbars, large covers, formed electrical enclosures, and low-to-medium volume production Full force throughout the stroke, adjustable pressure, controlled forming speed, and strong capability for deep forming Lower production speed, hydraulic heat and maintenance requirements, and generally higher cycle time than mechanical presses
Progressive Die Stamping Press 25–400 metric tons 60–1,000 strokes per minute, depending on part size, pitch, and material thickness Approximately 0.10–4.00 mm for continuous copper strip production Coil-fed line with a progressive die that performs multiple operations in one continuous sequence High-volume terminals, clips, contacts, busbar components, washers, and multi-feature electrical parts Combines several operations in one die, reduces handling, supports high output, and provides consistent part-to-part production High initial die cost, longer development time, and less economical for short runs or frequent design changes
Four-Column Hydraulic Press 100–2,000 metric tons 5–40 strokes per minute Approximately 1.00–15.00 mm for large or heavy copper components Large working area with guided moving platen; suitable for custom dies and multi-part fixtures Large busbars, transformer components, electrical cabinet parts, thick plates, and low-volume heavy forming Good working-area accessibility, even load distribution, adjustable pressure, and suitability for large tooling Large footprint, slower cycle speed, and more demanding installation and hydraulic maintenance requirements
Pneumatic Toggle or Bench Press 0.5–30 metric tons 20–120 strokes per minute, depending on cylinder size and operating mode Approximately 0.10–2.00 mm for light-gauge copper strip or sheet Manual loading, foot-switch operation, or simple automatic feeding for small parts Small terminals, light crimping, marking, light piercing, assembly support, and laboratory or maintenance work Compact design, simple operation, relatively low initial investment, and easy integration into small workstations Limited forming force and working area; unsuitable for large parts, deep drawing, or high-load production
CNC Turret Punch Press 20–300 metric tons equivalent punching force Approximately 200–1,200 hits per minute, depending on turret configuration and tool path Approximately 0.50–6.00 mm for copper sheet, subject to machine-rated thickness and tooling clearance CNC-controlled sheet handling with multiple indexed punching tools; typically used without dedicated progressive dies Prototype work, low-to-medium volume panels, electrical cabinets, ventilation parts, and varied hole patterns Fast setup for changing designs, flexible tooling, reduced need for dedicated dies, and good suitability for small batches Not normally the first choice for very high-volume small components or operations requiring extensive 3D forming

Typical ranges are provided for preliminary equipment comparison. Actual performance depends on copper grade, temper, strip width, part geometry, die clearance, lubrication, feed accuracy, and required production volume.

Key Specifications for Choosing the Best Machine in 2026

For global buyers, the best copper stamping machine in 2026 should match material thickness, part geometry, and production volume. The International Energy Agency’s Global Critical Minerals Outlook 2024 projects copper demand to rise from about 25 million tonnes in 2023 to more than 30 million tonnes by 2035 under stated policies. This pressure makes stable, efficient forming equipment increasingly important.

Check rated force, stroke length, shut height, and slide speed together. Peak tonnage alone can mislead. Ask for a force curve at your actual copper thickness. A 0.8 mm busbar may need different settings from a thin connector strip. Servo feeding should maintain repeatable positioning, ideally within the tolerance required by your drawings. Watch the feeder.

Energy use also matters. The U.S. Department of Energy reports that motor-driven systems consume a major share of manufacturing electricity. Compare motor efficiency, standby consumption, and recovery functions, not only purchase price. Useful specifications include automatic lubrication, overload protection, die sensors, emergency stopping, and accessible guarding. ISO 16092 guidance can support safer press design reviews. In factory trials, test burr height, springback, coil change time, and noise at full speed. A machine that reaches its advertised speed but damages edges is not a strong purchase. Request production samples, maintenance records, and independently verified accuracy data before approval.

How to Compare Copper Stamping Machine Performance and Costs

2026 Best Copper Stamping Machine for Global Buyers

Comparing copper stamping machines requires more than checking press force or purchase price. According to the International Copper Study Group’s 2024 market outlook, refined copper demand remains close to 27 million tonnes annually. This pressure increases the value of stable production and low material waste. Review stroke speed, feeding accuracy, die compatibility, and repeatability under continuous operation. A machine producing 80 parts per minute may outperform a faster model if rejects remain below 1%.

Cost comparison should include tooling, electricity, maintenance, labor, and downtime. The U.S. Energy Information Administration reports that industrial electricity prices vary widely between regions. Therefore, identical machines can create different operating costs in Asia, Europe, or North America. Request measured energy use per finished part, not only motor capacity. Also calculate payback using realistic utilization. Many quotations assume two or three shifts daily. That assumption may be wrong for seasonal factories. My own reviews often find that maintenance access matters more than a small difference in rated speed.

Tips: Ask for a sample run using your actual copper thickness and part shape. Record cycle time, scrap rate, noise, and temperature after several hours. Check spare-part availability and technician response times. The IEA’s Global Critical Minerals Outlook 2024 highlights rising copper demand from electrification. Efficient equipment should support growth without hiding repair costs. Do not trust one demonstration. Repeat the test.

Global Buying Guide: Suppliers, Standards, Shipping, and Support

For global buyers, choosing a copper stamping machine starts with supplier evidence, not attractive pricing. A reliable supplier should provide production records, machine drawings, test reports, and clear warranty terms. Ask for references from factories producing terminals, connectors, or precision copper parts. Request a live trial using your actual copper alloy, thickness, and die design. This reveals feeding problems early. The cheapest quote often hides costly adjustments.

Standards must match the destination market and factory conditions. Confirm electrical requirements, guarding, emergency stops, noise limits, and documentation. ISO 9001 certification can support quality control, but it does not replace machine-specific compliance. Ask which testing body issued each report. Check whether the control cabinet suits local voltage and frequency. Small details matter. I have seen projects delayed by incorrect plugs, missing manuals, and unclear spare-parts lists.

Shipping plans deserve the same attention as machine specifications. Confirm dimensions, gross weight, loading photos, moisture protection, and the agreed Incoterm. Request commercial invoices, packing lists, certificates of origin, and accurate tariff information. A wooden case should have suitable treatment marks where required. After arrival, technical support should include installation guidance, operator training, troubleshooting videos, and response times. Remote support is useful, but it cannot fix every setup mistake. Leave time for customs delays and commissioning adjustments; planning is never perfectly accurate.

Inquiry Form